
Advanced Mineral Processing & Global Export
Operating in Kankara, Katsina State, Nigeria
Precision-engineered extraction of Monazite, Zircon & Ilmenite — from raw earth to export-grade minerals.
Powering Global Supply Chains with Nigerian Minerals
Aadikal Cosmos Ltd is an advanced mineral processing and export enterprise headquartered in Kankara, Katsina State, Nigeria. We operate a fully integrated processing facility designed to extract and refine high-value minerals — Monazite, Zircon, and Ilmenite — from raw mineral sand deposits.
Our operations combine cutting-edge separation technology with scalable processing capacity, ensuring consistent output quality that meets the rigorous demands of international markets. We are committed to responsible sourcing, operational transparency, and building enduring partnerships across the global minerals trade.
Trust
Transparent operations with full investor visibility
Global Reach
Export-grade minerals meeting international standards
Scale
Industrial-capacity processing powered by advanced machinery
Precision
Multi-stage separation for maximum mineral purity

The Alchemical Pipeline
From raw earth to refined export-grade minerals — a five-stage precision extraction process engineered for maximum recovery and purity.
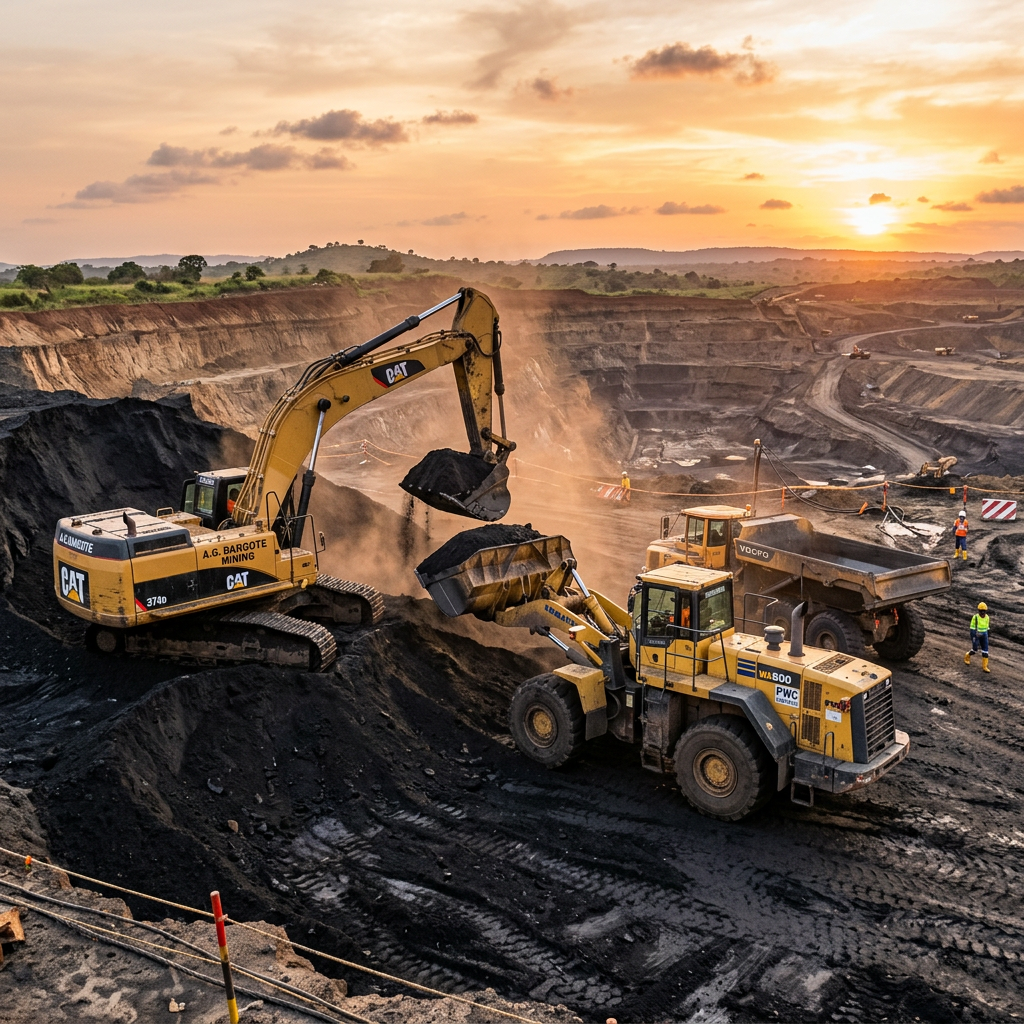
Raw Sand Sourcing
Mineral-rich sand is carefully sourced from designated deposits in Kankara using heavy excavators and front loaders, ensuring sustainable extraction of high-grade raw material.
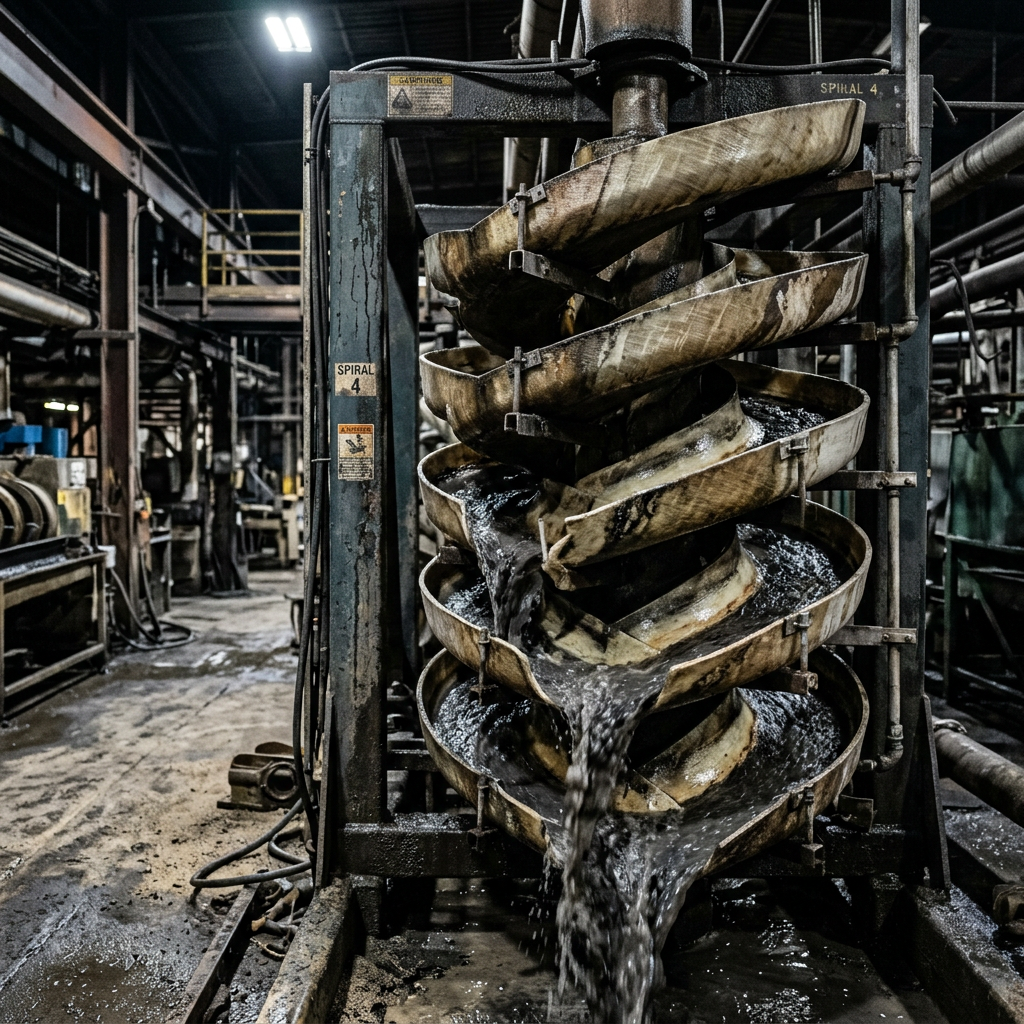
Spiral Separation
Gravity-based spiral chutes separate heavy mineral concentrates from lighter waste material using centrifugal force and water flow.
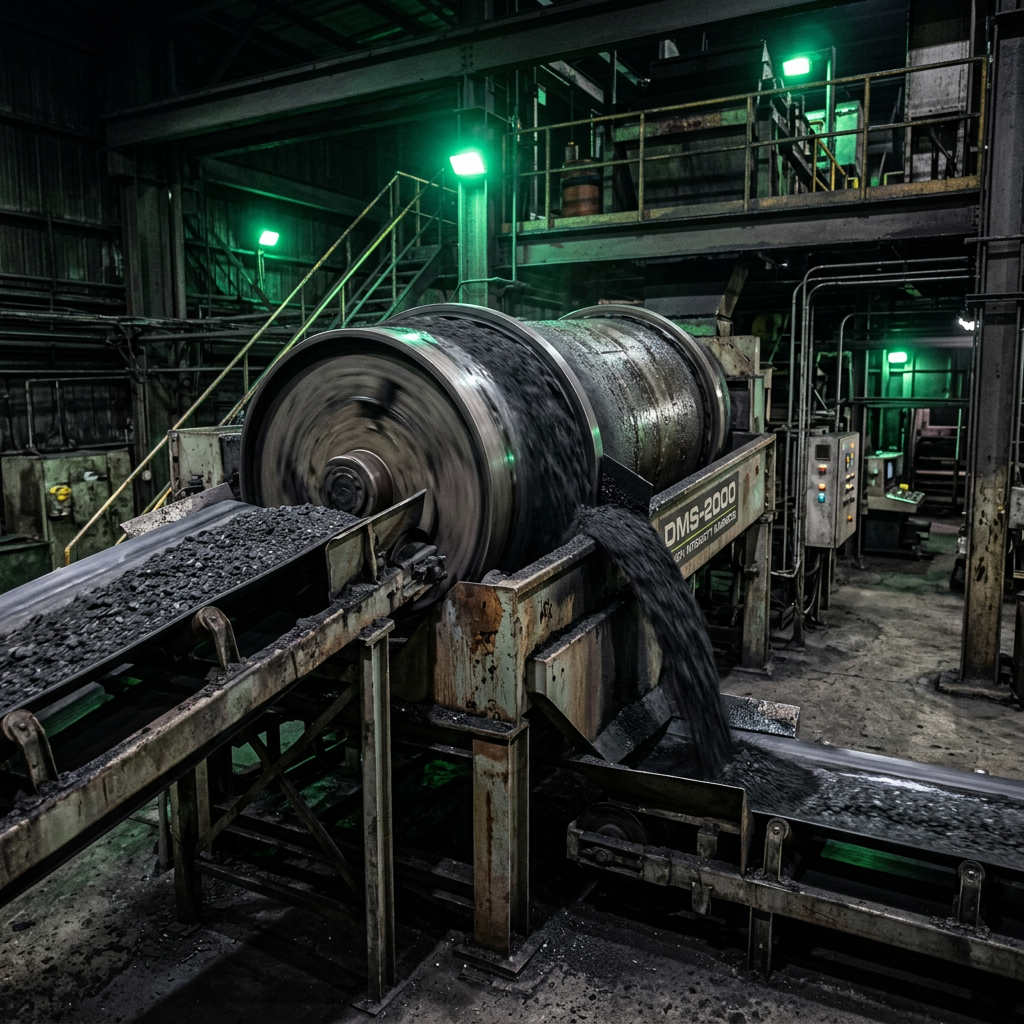
Magnetic Separation
High-intensity magnetic drums isolate iron-bearing minerals like Ilmenite from non-magnetic components with extreme precision.
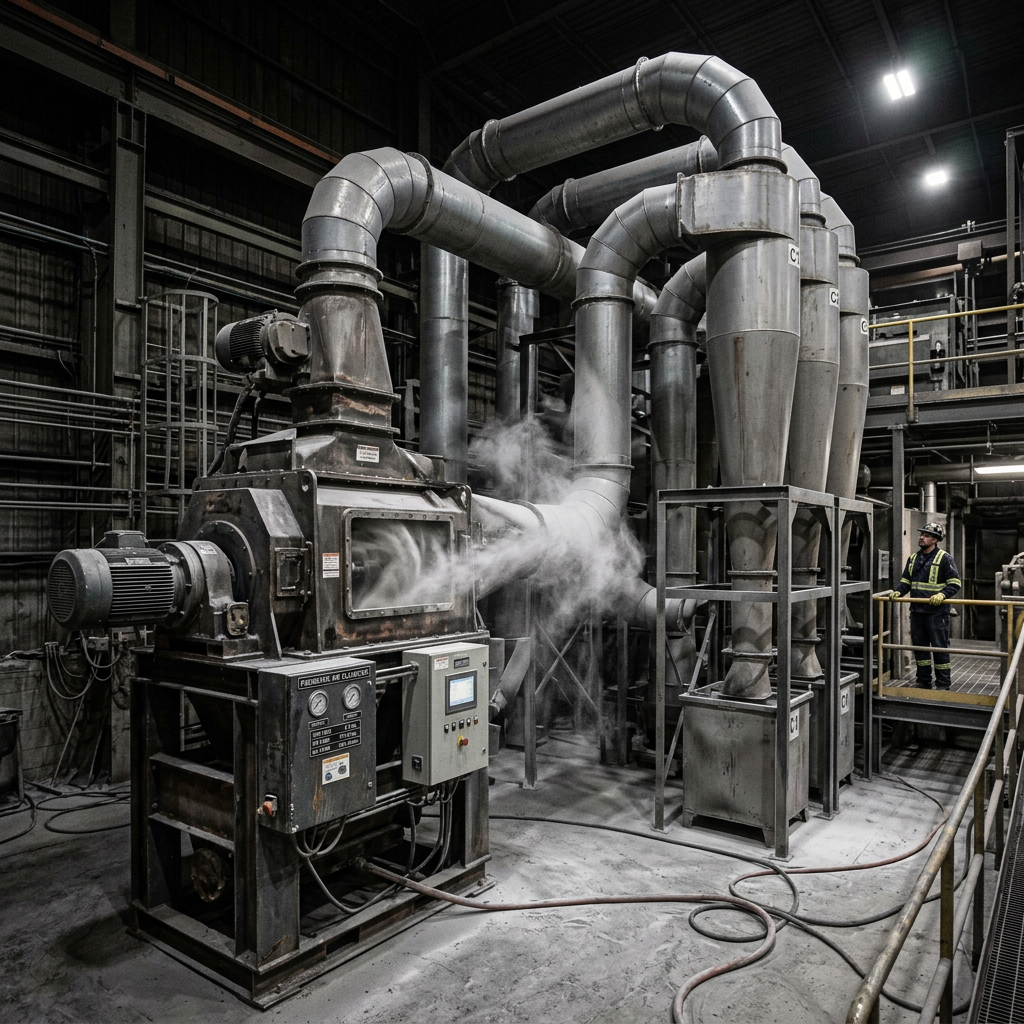
Airflow Separation
Advanced pneumatic classifiers use calibrated airstreams to separate minerals by density and particle size for final refinement.
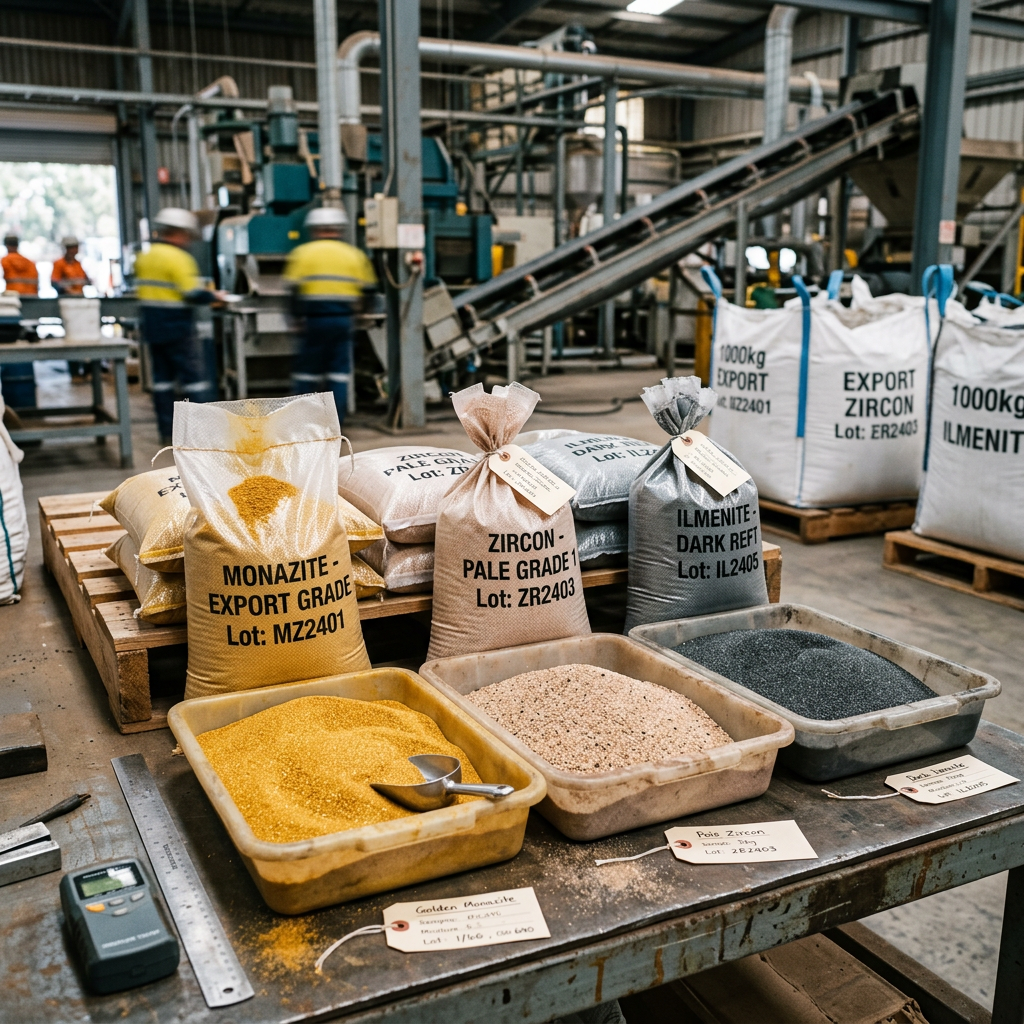
Final Mineral Extraction
Export-grade Monazite, Zircon, and Ilmenite are extracted at maximum purity — ready for international markets and industrial applications.
Industrial-Grade Equipment
Purpose-built processing machinery engineered for continuous high-capacity mineral extraction and refinement.
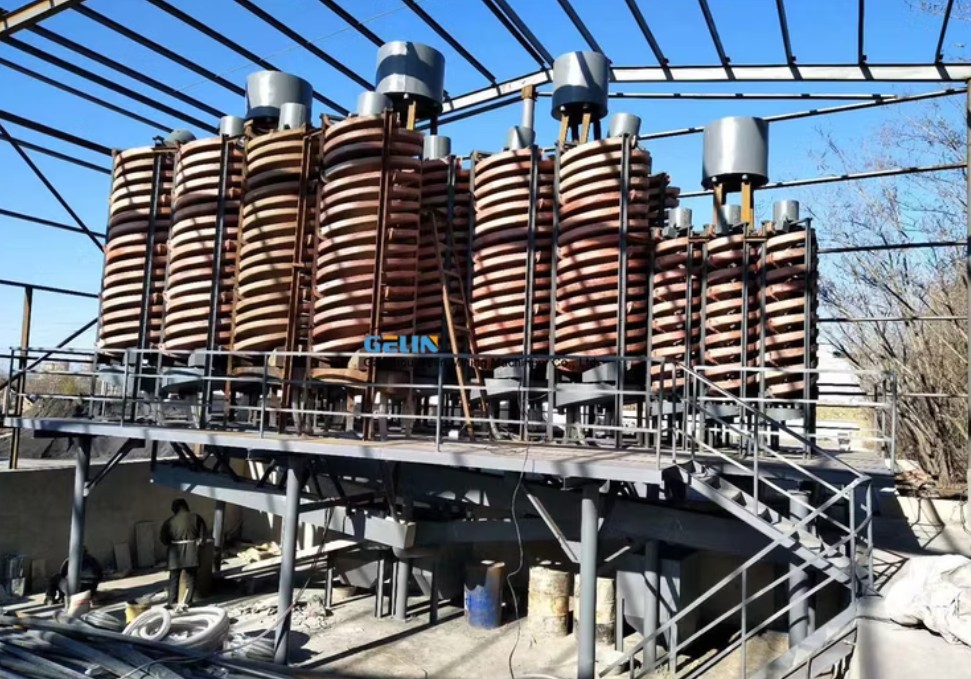
Spiral Chutes
High-capacity helical spiral separators utilizing gravity and centrifugal force to concentrate heavy minerals from raw feed slurry. Multiple spiral units operate in parallel for continuous, high-throughput processing.
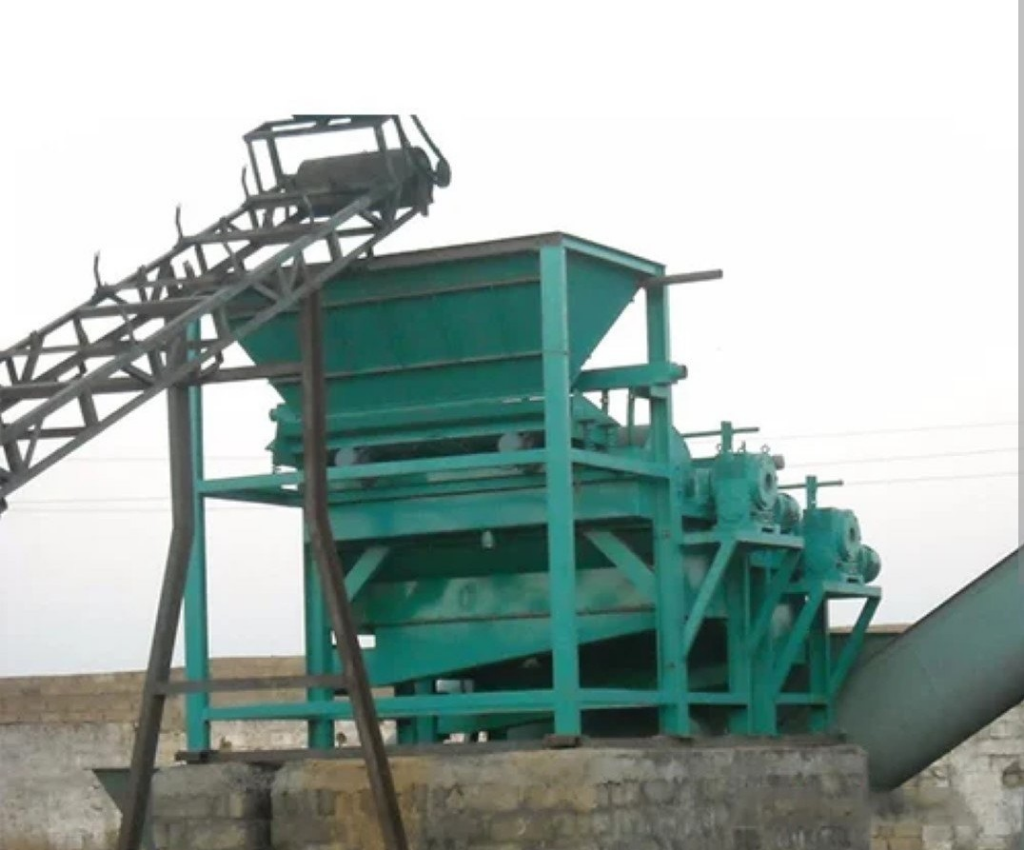
Magnetic Separator
Industrial drum magnetic separator with conveyor belt feed system for precise isolation of iron-bearing minerals like Ilmenite from non-magnetic fractions in the mineral concentrate.
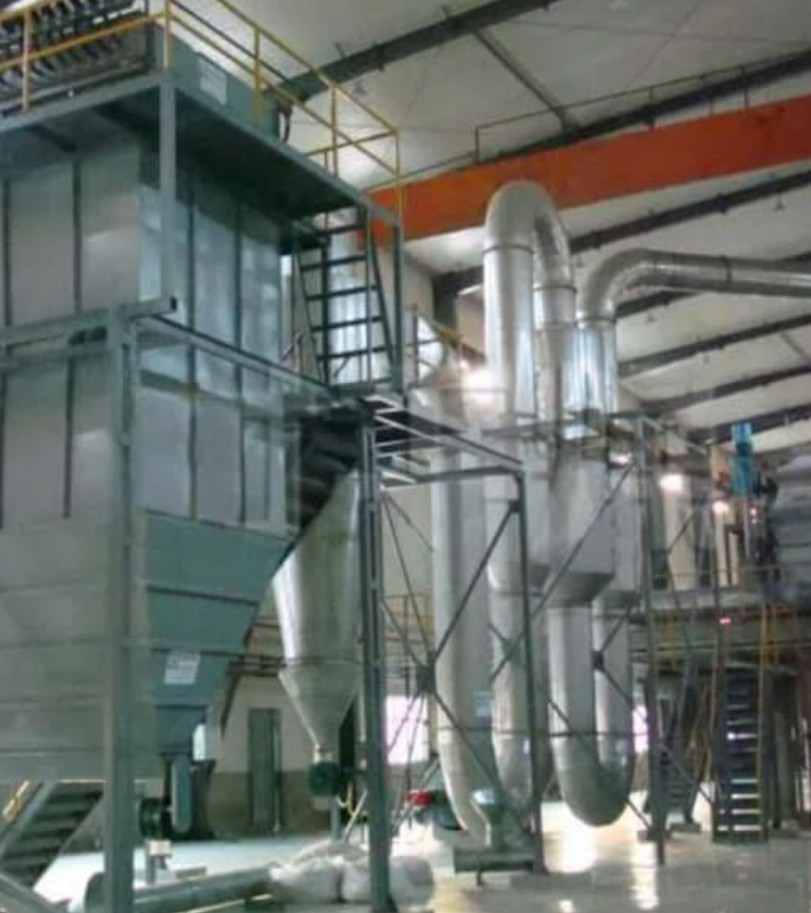
Airflow Machine
Advanced pneumatic classification system with cyclone separators and ducting networks that use calibrated airstreams to separate final mineral fractions by particle density and size.
Gold Extraction
A dedicated four-stage gold recovery circuit — from raw alluvial feed to export-grade gold concentrate, engineered for maximum recovery and purity.
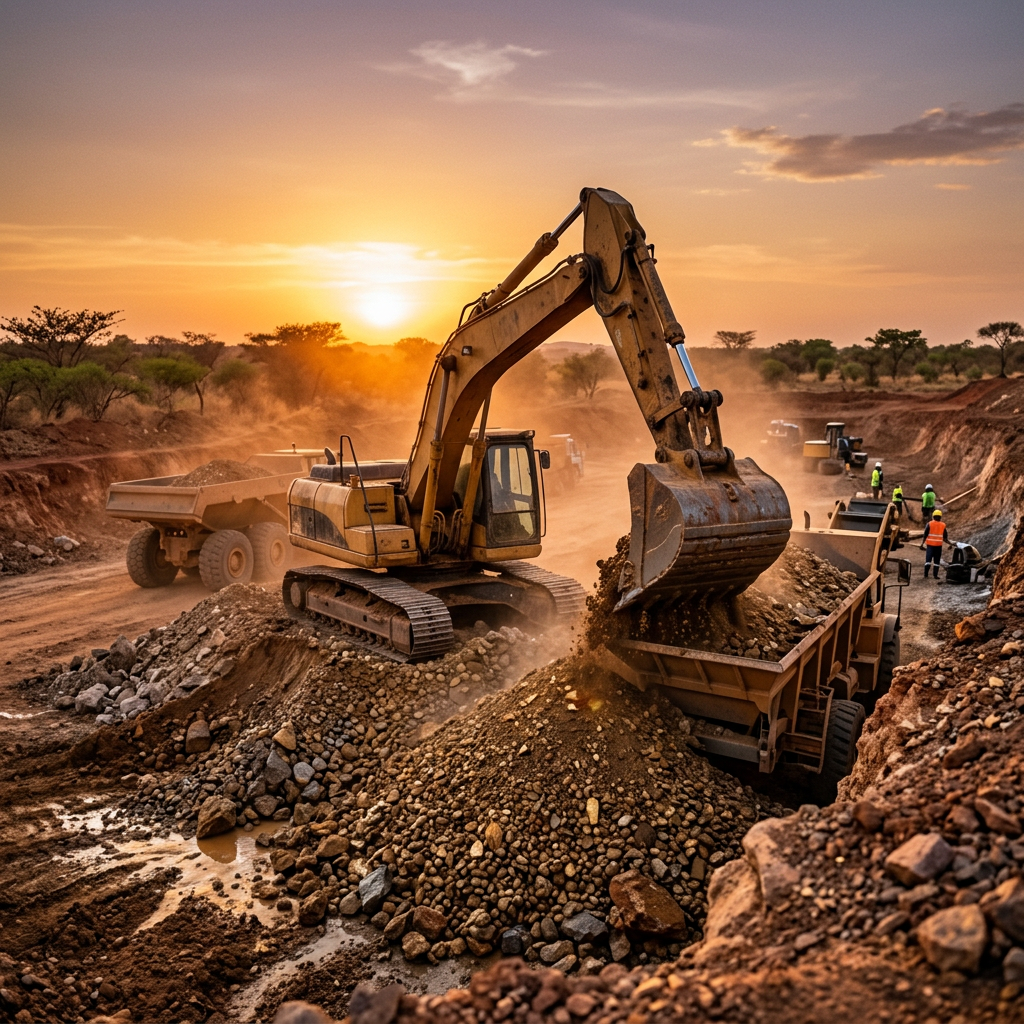
Gold-Rich Raw Material Sourcing
Alluvial gold-bearing gravel and ore is extracted from designated deposits using heavy excavators. Our geologists identify high-yield zones to maximise recovery from every tonne of raw material processed.
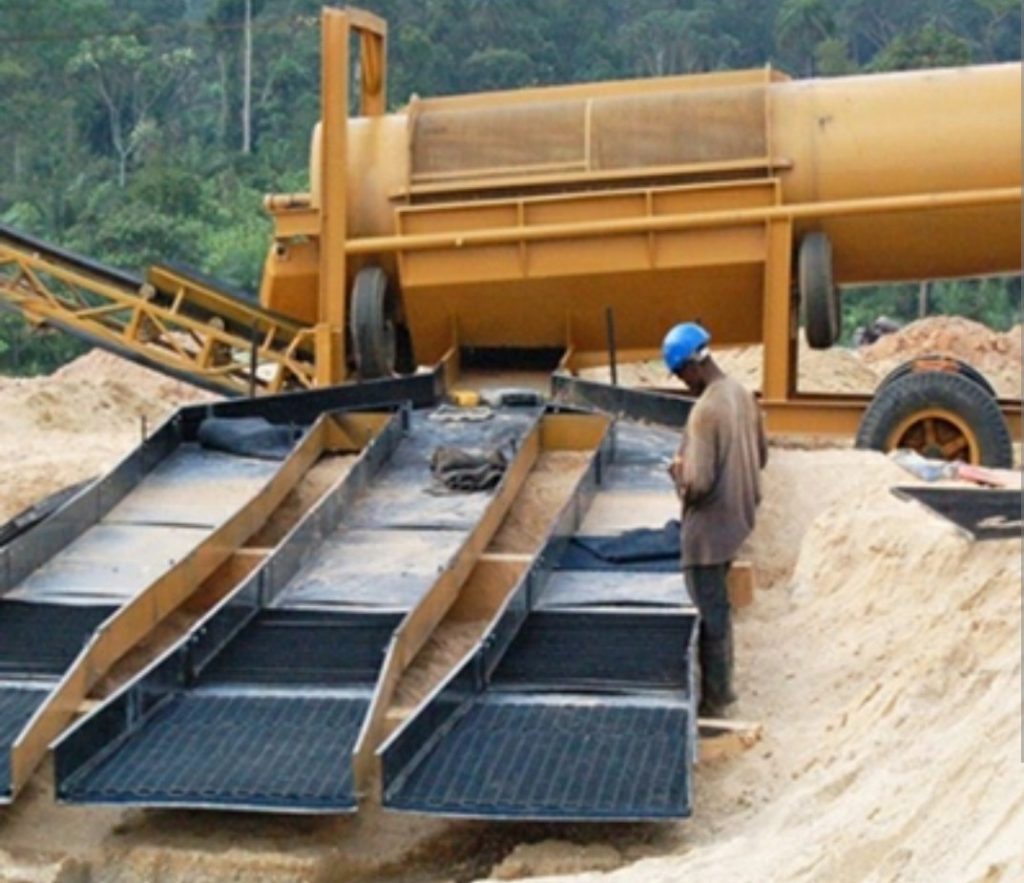
Sluice Machine Recovery
High-capacity sluice machines process raw feed material with pressurised water flow over riffled recovery mats, capturing coarse and mid-size gold particles in the initial concentration stage.
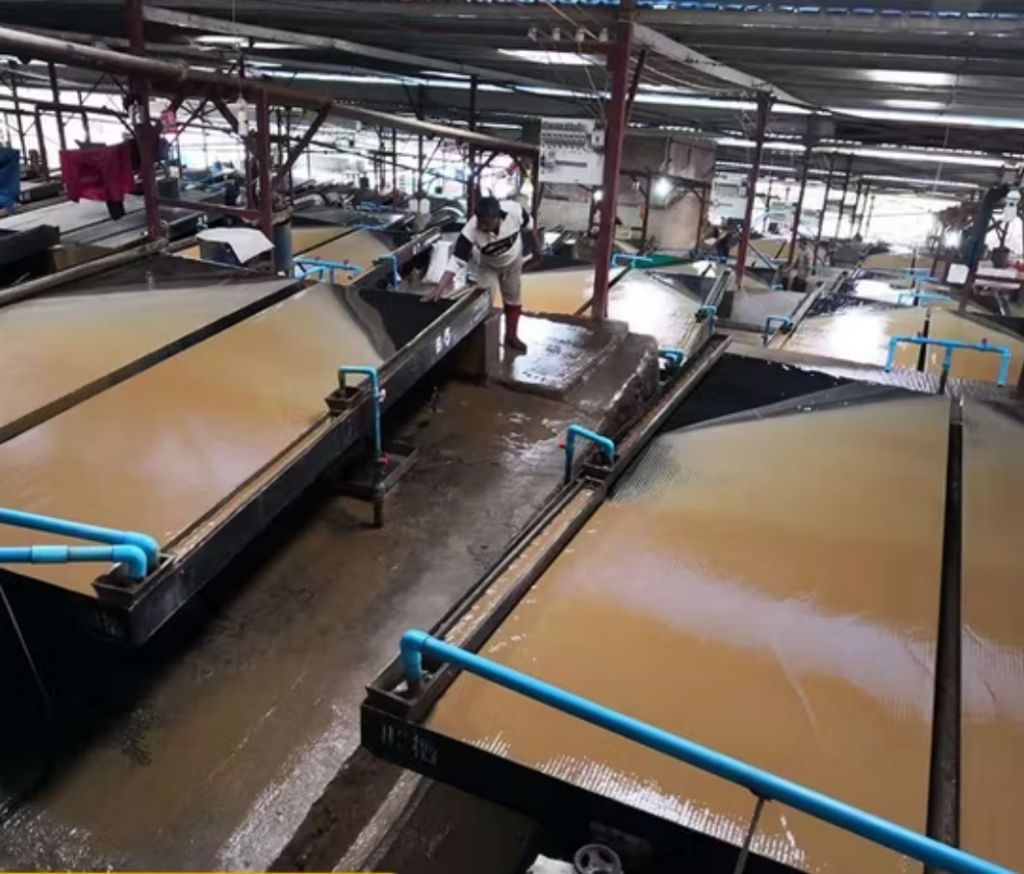
Shaking Table Fine Separation
Precision shaking tables refine the sluice concentrate further, using controlled vibration and water flow to separate fine gold particles from remaining sand and gangue material with exceptional accuracy.
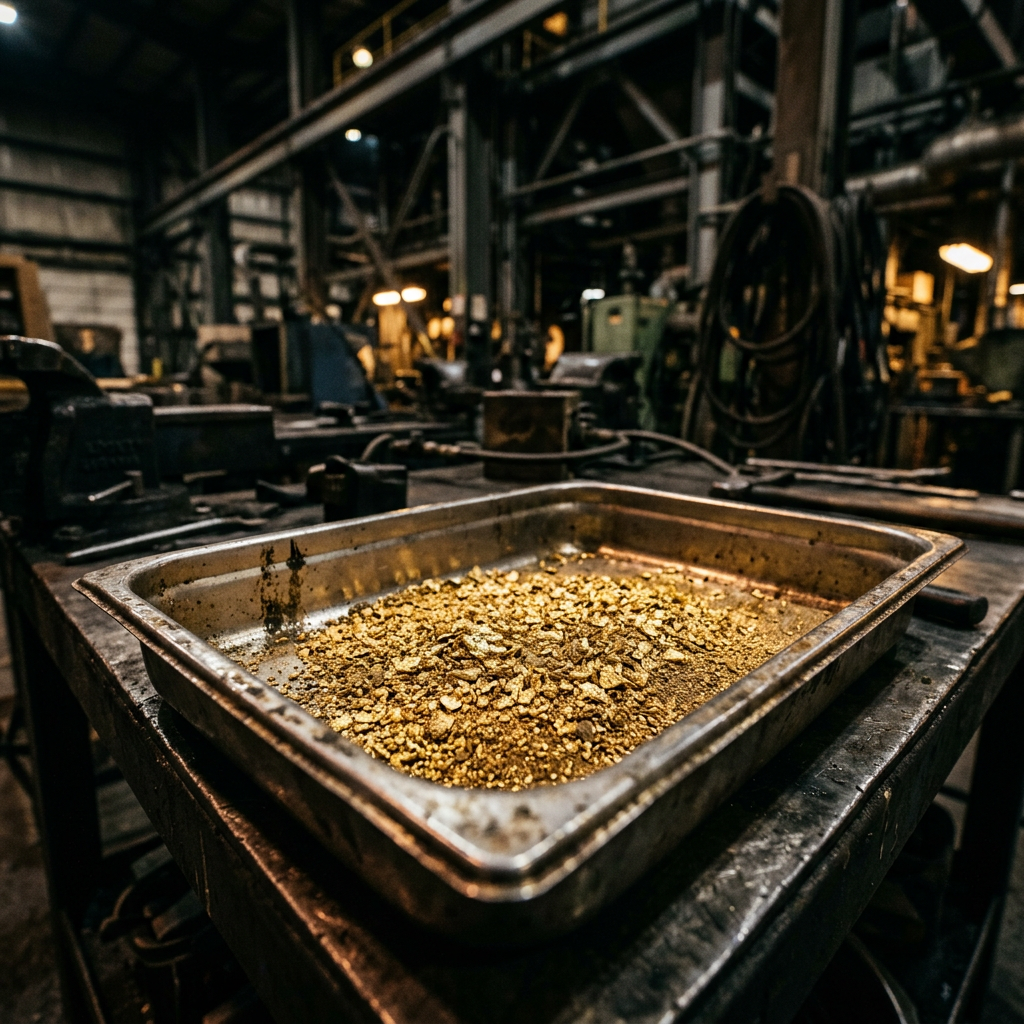
Final Gold Concentration & Export
The final gold concentrate is cleaned, weighed and packaged to international export standards. Each batch is assayed for purity before dispatch to our global buyers and refineries.
Export-Ready Minerals
Four high-value mineral concentrates extracted and refined at our Kankara facility, ready for global industrial markets.
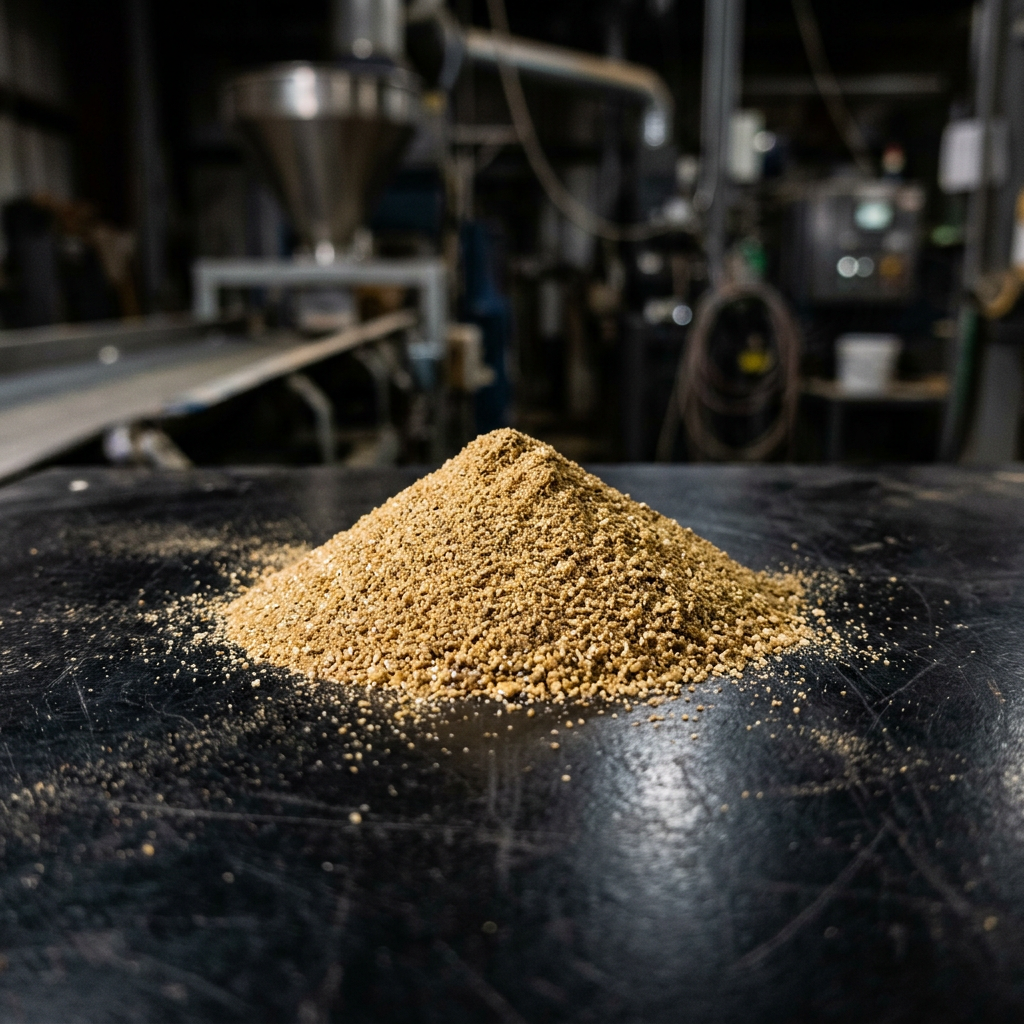
Monazite
Rare-earth phosphate mineral rich in cerium, lanthanum and thorium. Used in electronics, catalysts, and advanced materials manufacturing.
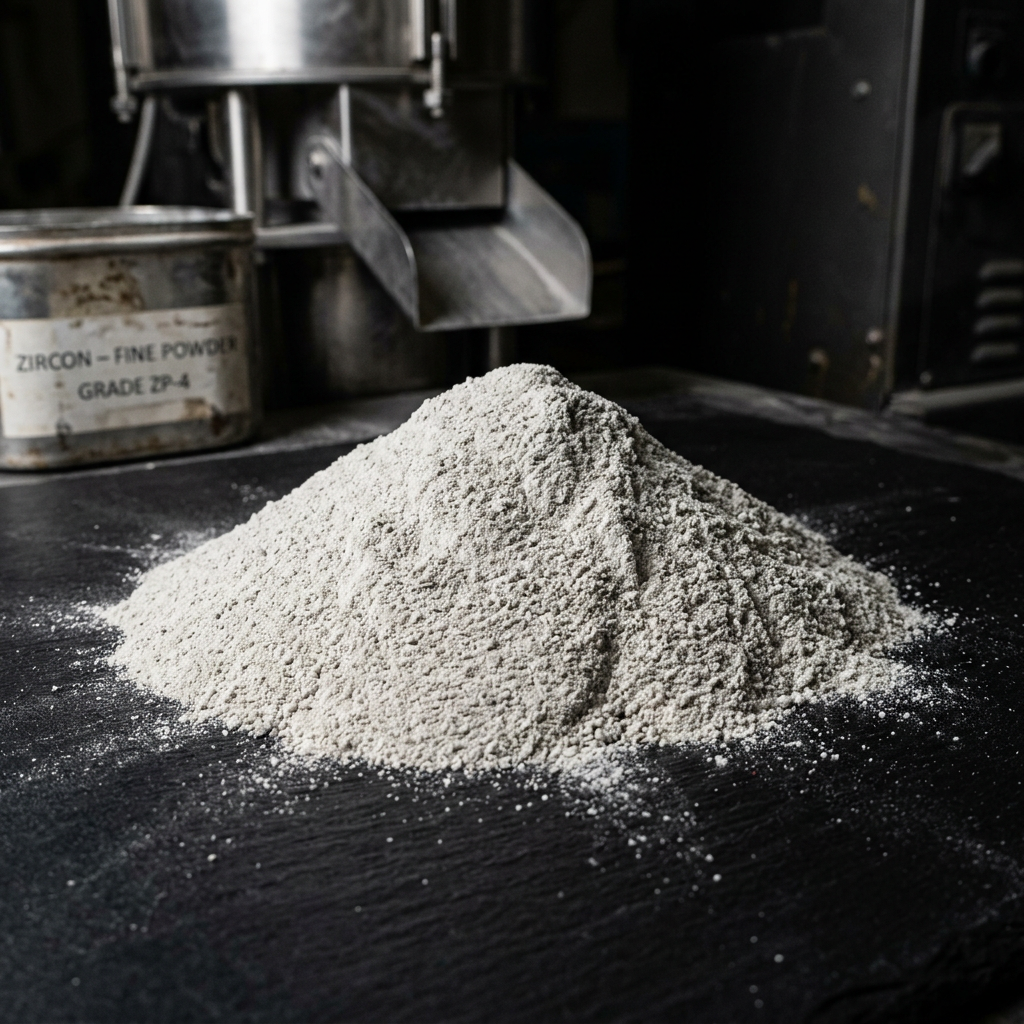
Zircon
Premium zirconium silicate concentrate prized for its exceptional heat resistance, chemical stability and use in ceramics and foundry applications.
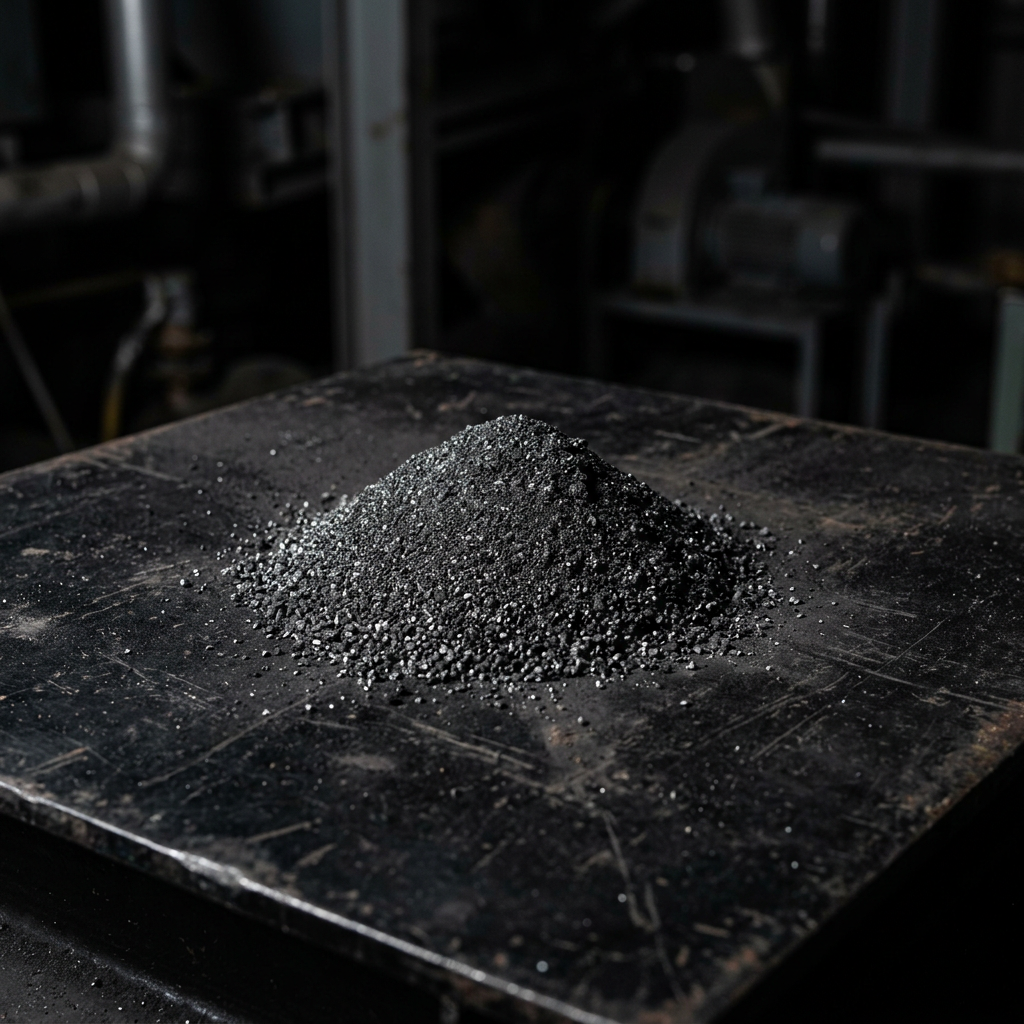
Ilmenite
Iron-titanium oxide mineral; primary feedstock for titanium dioxide pigment production used globally in paints, plastics and paper industries.
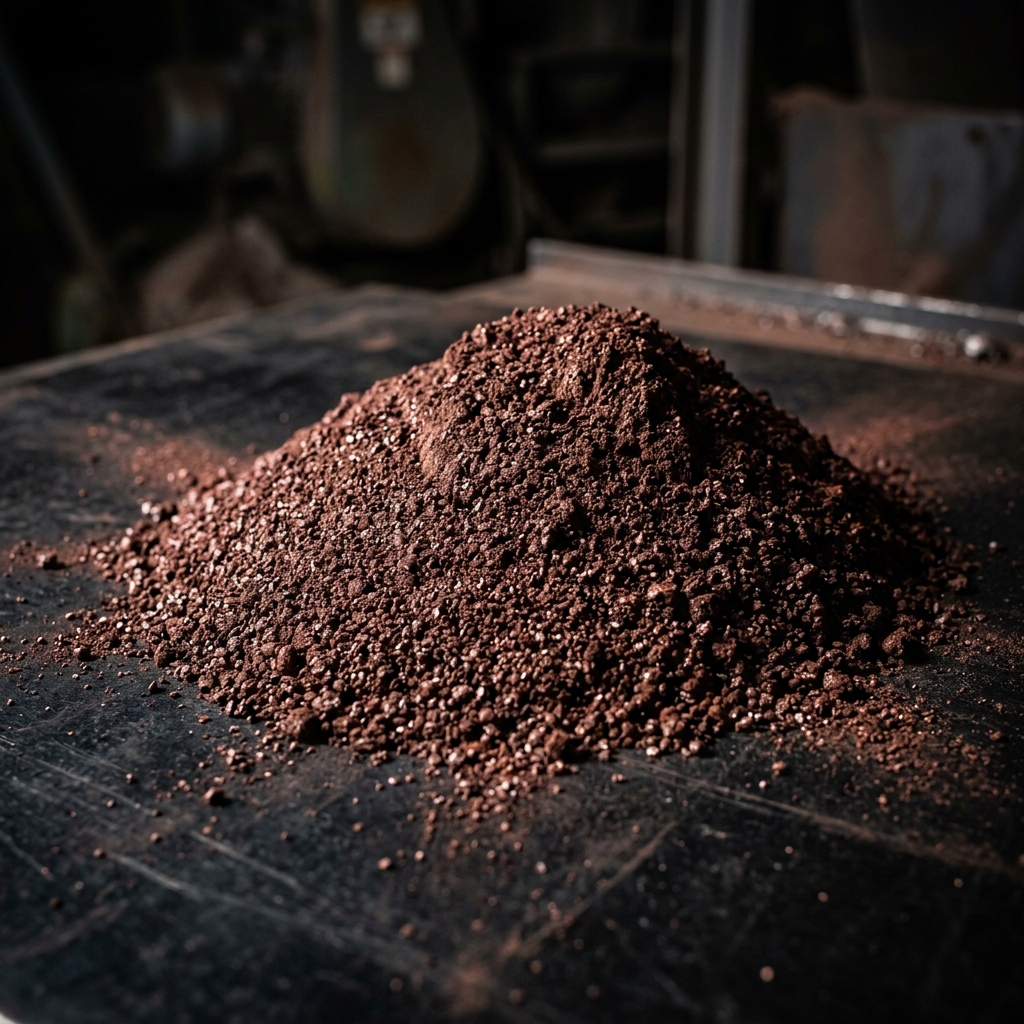
Iron Concentrate
High-grade iron concentrate separated from mineral sands processing. Supplied to steel mills and foundries for direct use in iron and steel production.
Live Operations
Real-time visibility into our processing facility. Radical transparency for investors and partners.
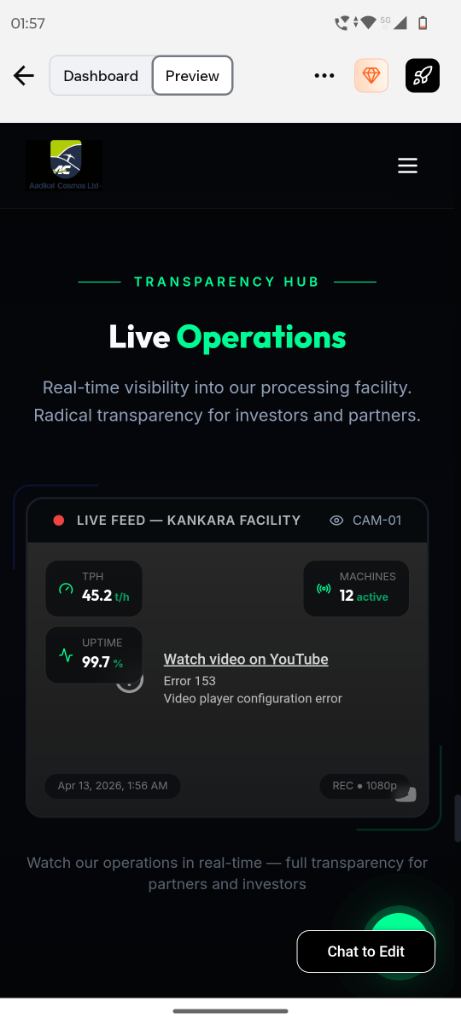
Watch our operations in real-time — full transparency for partners and investors
Built for Performance & Trust
Every element of our operation is optimized for maximum mineral recovery, operational reliability, and client confidence.
High Recovery Efficiency
Our multi-stage extraction pipeline achieves 95%+ mineral recovery rates, maximizing value from every ton of raw feed material.
Scalable Processing (TPH)
Industrial-capacity throughput engineered to scale with demand. Our facility handles high-volume processing around the clock.
Trusted Sourcing
Ethically sourced mineral deposits with full chain-of-custody documentation. Complete operational transparency for all stakeholders.
Export-Ready Minerals
Refined Monazite, Zircon, and Ilmenite processed to international purity standards, packaged and certified for global export.
Ready to Partner With Us?
Whether you're an investor, buyer, or partner — we're ready to discuss how Aadikal Cosmos can serve your mineral supply needs at scale.
Contact Us Directly
Reach our team instantly via WhatsApp for inquiries about mineral supply, partnerships, or investment opportunities.
Chat on WhatsAppAvailable Mon - Sat, 8AM - 6PM WAT
Monazite Percentage Calculator
Enter your sample results to calculate the monazite percentage and estimate yield per kilogram of sand.
Monazite Percentage
2.00%
2g per 100g of sand
Expected Yield
0.02kg
monazite in 1kg of sand